Converters compare jumbo rolls on rate per kilogram because that number is easy to get. The number that decides profitability is yield - the proportion of the roll that leaves your slitter as saleable finished tape. Six characteristics determine that yield, and none of them appear on a price list.
Coating uniformity across the web
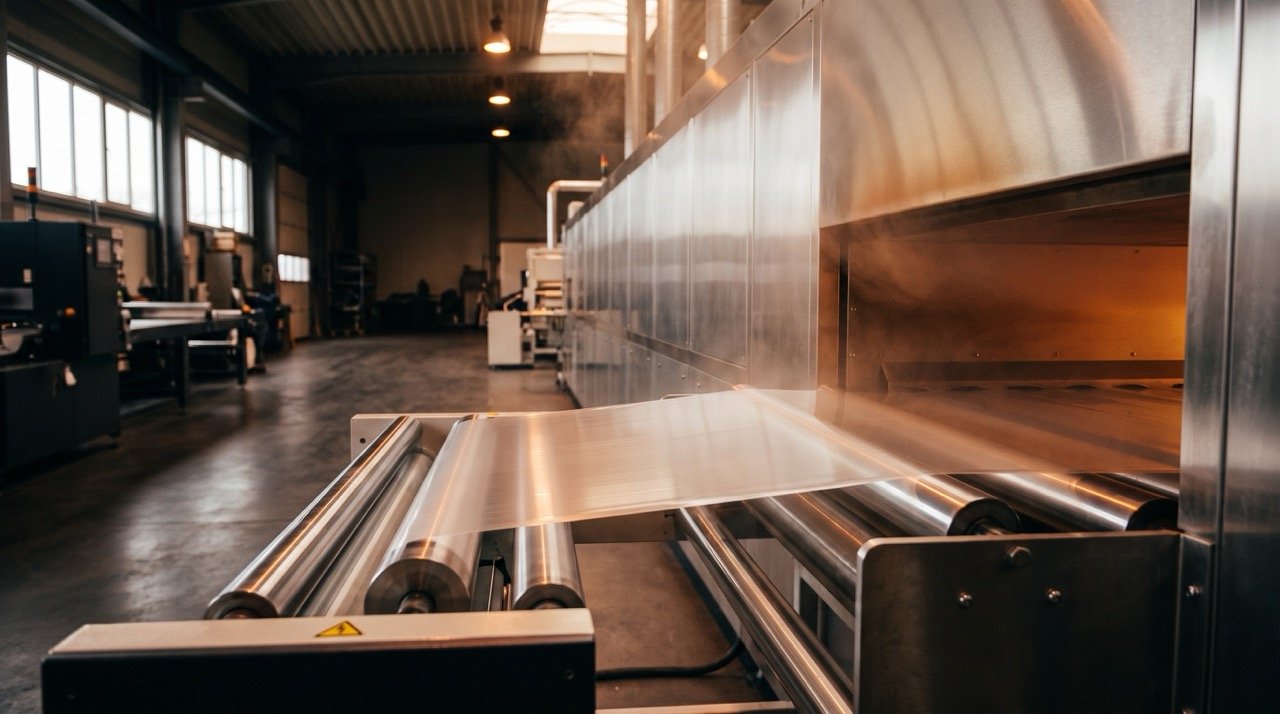
Adhesive deposited unevenly across the width produces finished rolls with different peel values depending on where in the parent roll they were cut. Your customer receives inconsistent tape from what you correctly believe is a single batch.
Ask for coat weight readings taken at multiple points across the web, not a single centre-line figure. A supplier who measures across the width is controlling the variable that matters to you.
Edge quality and how it decides trim loss
Wavy, gummed or damaged edges have to be trimmed away before slitting. Every millimetre trimmed is material you paid for and cannot sell, and the loss repeats on every roll you buy.
Clean, straight, burr-free edges also matter downstream: a rough edge starts a tear that propagates through the finished roll, and the customer sees it as a quality defect in your product.
Winding tension and roll structure
A jumbo wound too tightly cold-flows over time - the adhesive migrates and the roll develops hard and soft bands. Wound too loosely, the roll telescopes in transit and arrives with a stepped edge that cannot be slit cleanly.
Inspect the roll face on arrival. A flat, even face with no telescoping and no visible banding indicates controlled tension. A dished or stepped face is a warning that runs before the first metre is unwound.
Core specification and diameter
Core internal diameter has to match your shafts, and core wall strength has to survive the chucking pressure without crushing. A crushed core means the last several layers of an expensive roll are scrap.
Confirm core diameter, wall thickness and material before the first order, not after the first delivery. Paper cores also need to be dry - a core that has absorbed moisture in storage loses crush resistance.
Batch documentation and traceability
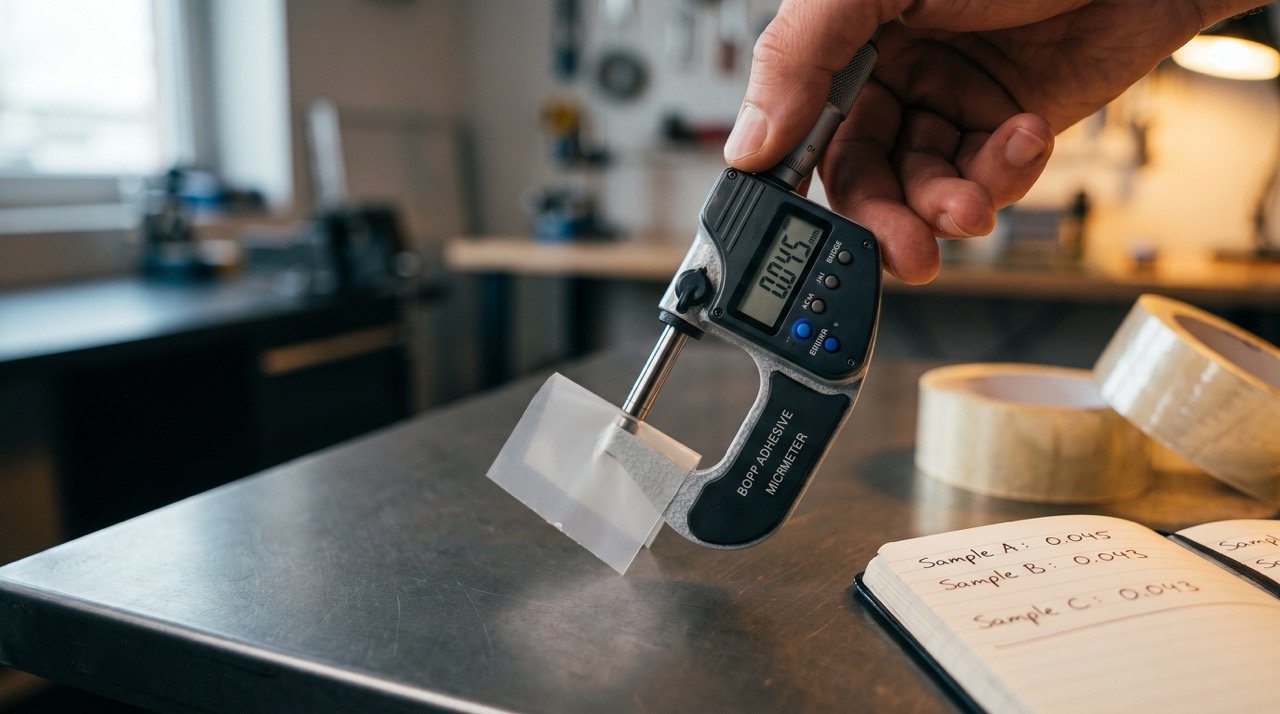
A test report should accompany each batch with peel adhesion, tensile strength, elongation and thickness, along with the batch number and production date. Without it, you cannot answer your own customer when they query a roll.
Traceability is what lets a problem be contained to one batch instead of triggering a blanket recall of everything you shipped that month.
Working the economics backwards
Take the delivered price per kilogram and divide by your realised yield after trim, splices and start-up waste. A cheaper roll at 88 percent yield costs more per saleable metre than a better roll at 96 percent, and the gap widens with every splice your operators have to work around.
Count splices per roll as part of the specification. Each one costs machine downtime and produces scrap around the joint.
Questions We Are Asked About This
We supply BOPP and double-sided tissue jumbo rolls in widths up to 1300 mm, with lengths matched to your slitter capacity.
Yes. Every dispatch carries batch-wise peel adhesion, tensile, elongation and thickness data with the batch number recorded.
We would prefer you trial before committing. Trial rolls let you measure realised yield on your own slitter, which is the only number that settles the comparison.